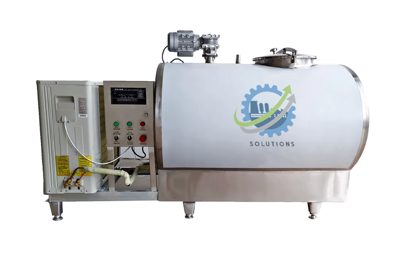
Double-Jacketed Tank

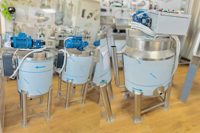
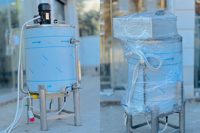
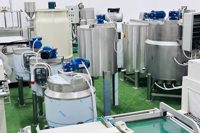
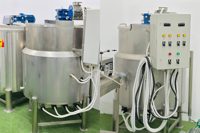
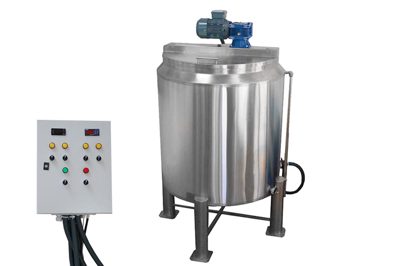
Double-Jacketed Tank
Product:
Double-jacketed tank
Manufacturer:
Al Atheer Industrial Solutions
General description:
The double-jacketed tank is a basic piece of industrial equipment on production lines that require precise temperature control of materials, whether by indirect heating or cooling.
This type of tank is used in many sectors such as the food, pharmaceutical and cosmetic industries, as well as in chemical applications and research.
The tank works on the principle of two parallel walls (double wall): the inner wall holds the material to be processed, while the heating medium (such as hot water or steam) or cooling medium (such as cold water or glycol) passes through the space between the walls.
This system maintains a constant, uniform temperature inside the tank without the material ever touching the heat or cooling source directly, ensuring safety and quality in the production process.
Structure and design:
-
The tank is made entirely of rust-resistant food-grade stainless steel of type SUS304 or SUS316 on request.
-
All parts are welded precisely to prevent liquid leaks or heat loss.
-
The inner surface is mirror polished to reduce sticking and ease cleaning.
-
The outer surface is polished or matt according to the customer's requirements.
-
Fitted with a tight top lid that opens easily for inspection or filling.
-
The tank base can be fixed or on castors depending on the working environment.
Operation and control system:
-
Option of temperature control through a digital panel showing the live reading and the heating or cooling rate.
-
Includes a temperature indicator (thermometer) and aprecise temperature sensor inside the inner wall.
-
A thermostat or pressure regulator can be integrated to protect the system from any unwanted rise in temperature or pressure.
-
Option of adding a circulation pump for hot or cold water to improve uniform heat distribution around the tank.
Optional extras (on request):
-
Mechanical or magnetic mixing system for viscous or liquid materials.
-
High shear homogenizer to blend ingredients and produce fine, even mixing.
-
A third jacket with heat insulation to reduce heat loss and increase system efficiency.
-
Internal electric heaters or an external boiler as the heat source.
-
Integrated cooling system based on an external chiller or a built-in cooling unit.
-
Bottom stainless steel drain valve to empty the contents easily.
-
Liquid level gauges or digital sensors to control the quantity.
-
Option of a CIP (clean-in-place) port to ease internal washing and sanitising.
Material:
All parts are made of rust-resistant food-grade stainless steel and comply with international food and pharmaceutical safety standards such as GMP and FDA.
The tank can be supplied in different materials depending on the application, such as SUS304 for food products or SUS316 for highly reactive chemicals.
Capacity options:
The tank is made in different capacities as needed, including the standard sizes:
-
100 litres
-
500 litres
-
1000 litres
The tank can also be designed with a custom capacity based on the customer's requirements and the nature of the industrial use.
Safety system:
-
Fitted with a safety valve to relieve excess pressure.
-
A control system that prevents operation if the permitted temperature limits are exceeded.
-
A fixed base or anti-slip castors with a locking system to hold the tank during operation.
Applications:
-
Food industries: preparing sauces, chocolate, dairy, concentrated juices and liquid batters.
-
Pharmaceutical industries: preparing creams, ointments and medical solutions.
-
Chemical industries: mixing oils, sanitisers and liquid detergents.
-
Cosmetic industries: producing shampoo, lotion, creams and perfumes.
Note:
This product is designed and manufactured to order to suit the required application in size, mixing type, and heating or cooling system.
The Al Atheer Industrial Solutions team can adapt the design to the specifications of the customer's plant or production line to guarantee the highest efficiency and performance.